
Blackbird client Atlas Copco Tools & Industrial Assembly Solutions was invited to share its insight for MEPCA magazine:
Manufacturers have never had access to more production data. Yet the commercial value of that information depends on how effectively it can be translated into insight, enabling better decisions about quality, productivity, cost and future investment. As AI accelerates, there are some important questions surrounding this dearth of data. Perhaps the biggest of which is not simply how much data are manufacturers collecting but rather are they making use of what they already have?
Factories generate enormous quantities of information, from assembly parameters and quality inspection results to equipment performance and production traceability. This data can help explain what is happening at specific points in the process, but they are often isolated in specific machines or siloed systems. When connected, however, they can provide a much broader understanding of the whole assembly process, why performance varies, where resources are being lost and which interventions are likely to deliver the greatest commercial return.
Connecting the dots
One of the persistent barriers to achieving this is fragmentation. Manufacturing operations frequently rely on multiple machines, controllers, software platforms and inspection systems, each generating information within its own environment. When these systems operate in isolation, data is ‘trapped’, so understanding performance across an entire production process becomes more difficult.
This is certainly an area where manufacturers need to challenge their own assumptions. For example, if data is being collected to monitor a machine, are we also using it to understand product quality? If quality information is being captured, can it help explain production variation? If a process is generating information about downtime, can that data help inform decisions about maintenance, workforce skillsets or capital investment?
A connected manufacturing environment creates opportunities to combine process information with quality and production data, giving decision-makers a more complete picture. Instead of examining an isolated fault or a single machine’s output, teams can investigate relationships between process parameters, product quality, downtime and production efficiency. This changes the nature of decision-making. Maintenance teams may be better equipped to identify emerging problems; quality engineers can investigate the causes of defects more effectively; and production managers can make more informed choices about capacity, resources and process improvements.
The commercial benefit comes from acting on those insights. Reducing rework, avoiding unnecessary downtime, improving throughput and making better use of materials all have implications for operating costs and profitability. Equally, reliable production data can support more confident decisions about capital expenditure and the introduction of new manufacturing processes.
AI is only as useful as the questions we ask
Artificial intelligence offers significant potential to accelerate this process, but its effectiveness depends on the quality and context of the information available to it. AI cannot reliably compensate for disconnected systems, inconsistent data or an unclear understanding of the manufacturing process it is intended to improve.
This means manufacturers may need to think carefully about where AI is applied. The obvious opportunity might be automating an existing task, but the greater commercial value could lie elsewhere. In quality assurance, for example, AI-enabled vision systems can identify defects, recognise components and provide robotic guidance with AI. But the information generated can potentially do more than automate inspection. Analysed over time, it can help manufacturers understand patterns of variation, improve process consistency and reduce waste.
The same principle applies before production even begins. Atlas Copco’s Machine Vision solution, for example, can use three-dimensional CAD models to generate synthetic images for training machine vision applications. This creates an opportunity to identify potential problems earlier and prepare for product variants before physical production samples are available.
The lesson here is broader than any individual technology. If manufacturers can generate and analyse meaningful information earlier in the production lifecycle, they can potentially make better decisions before significant resources have been committed.
The smart factory is an ecosystem, not a collection of technologies
The fundamental prerequisite is that data has to be accessible and meaningful across the manufacturing ecosystem. For manufacturers operating complex assembly lines, the significance extends beyond simplifying machine control. A more consistent approach to data access can reduce integration complexity and help establish a clearer view of processes across the factory.
This is where the concept of the smart factory becomes particularly relevant. A genuinely connected manufacturing environment creates the foundations for information to move beyond individual machines and departments, allowing insight to be generated across the wider production process.
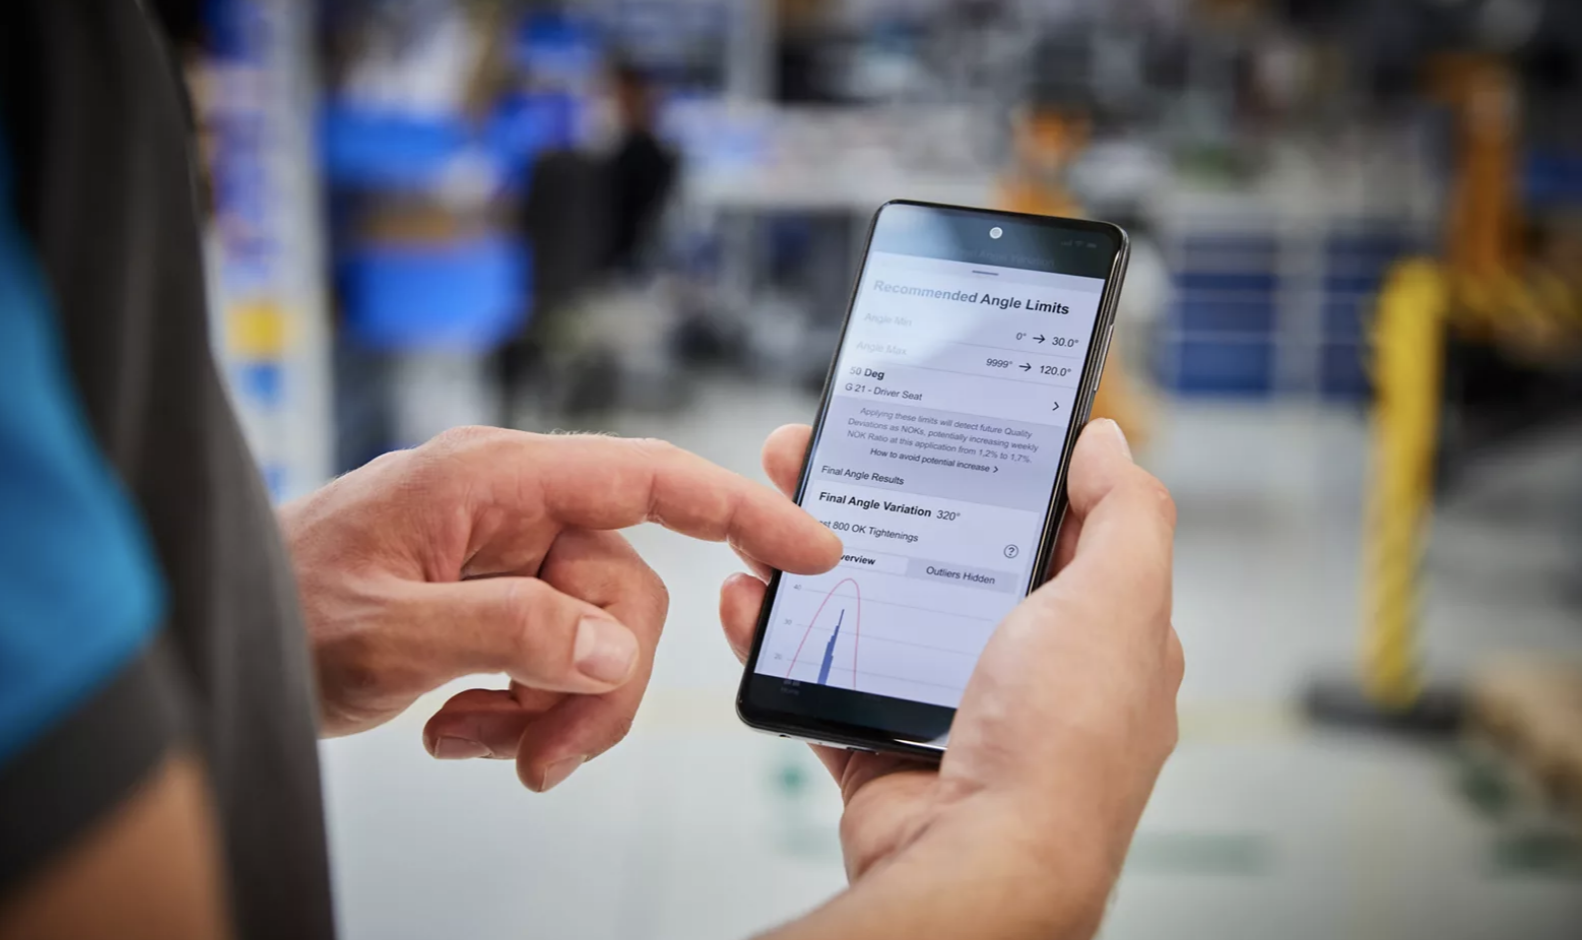
Atlas Copco’s ALTURE is an example of what is possible when that ecosystem is already in place. The system applies advanced analytics and machine learning to production data from smart tooling and controllers, using it to identify emerging risks, tightening trends and potential quality issues. Rather than simply presenting another set of production statistics, it is designed to turn those signals into actionable information and recommendations.
The important point, however, is that solutions such as ALTURE do not exist in isolation. Their value depends on having smart manufacturing infrastructure in place, including connected tools, controllers, software and data.
For manufacturers looking at their digital transformation, this raises another useful question: “are we investing in individual smart technologies, or are we building an ecosystem in which those technologies can work together?”
The importance of looking at the whole picture
Technology should not become an end in itself. The ultimate question for manufacturers is to consider what you would do differently as a result of the information you have.
Does the insight enable a defect to be prevented rather than detected? Does it allow maintenance to be planned rather than reacted to? Does it identify a bottleneck that had previously been overlooked? Does it demonstrate that a capital investment is genuinely necessary? These are the questions that turn data into commercial value.
There is also a sustainability dimension. Less scrap and rework mean fewer wasted materials and less unnecessary processing. Better operational insight can reveal inefficiencies and support more considered decisions about energy use, production planning and resource utilisation.
Achieving these outcomes requires collaboration between engineering, operations, IT and business leadership. Technical teams understand the processes and their limitations; data specialists help turn information into usable analysis; and commercial leaders must ensure that the resulting insight addresses genuine business priorities.
People remain central to this model. Whilst AI can identify patterns and provide recommendations, human expertise still is essential for interpreting results, assessing risk and deciding how to respond. Manufacturers will also need to develop workforce skills as digital technologies become more embedded in everyday operations.
Comments are closed.